

Retort packaging must do more than withstand high temperatures. It also needs to maintain a reliable seal throughout heating, cooling, storage, and transportation. Even when the packaging material provides strong barrier protection, a weak or inconsistent seal can allow moisture, air, or microorganisms to enter the package and compromise the product.
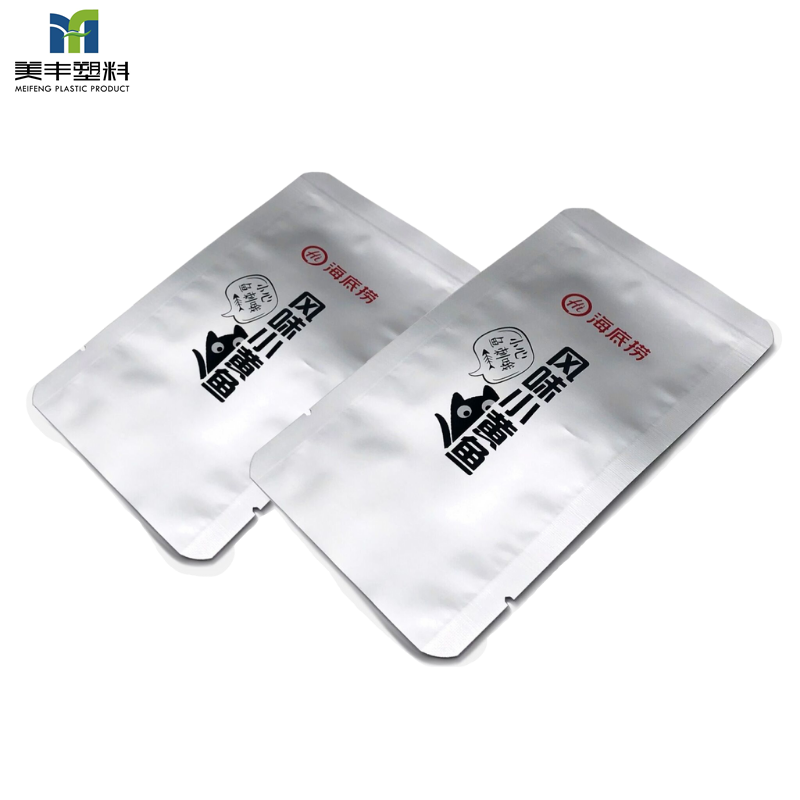
For food manufacturers using Retort Aluminum Foil Flat Pouches, seal integrity is therefore a critical part of packaging performance. Problems may originate during filling and sealing, become more visible during retort processing, or appear later when finished pouches are handled. Understanding where these problems begin helps improve packaging reliability without relying on unnecessary material changes.
Why Seal Integrity Matters in Retort Packaging
A retort pouch is exposed to demanding conditions during thermal processing. Temperature and pressure change throughout the heating and cooling cycles, while the product inside may expand or shift. The seal must remain intact despite these mechanical and thermal stresses.
Unlike a package used only for ordinary storage, a retort pouch must maintain its sealing performance after exposure to its specified processing conditions. If the seal weakens, the package may lose its protective barrier even when the laminated body remains undamaged.
This is particularly important for products with extended shelf-life requirements. A small channel in the seal may not be immediately visible, but it can provide a pathway for leakage or contamination. For this reason, evaluating Retort Aluminum Foil Flat Pouches requires attention to both the laminated structure and the finished seal.
Common Seal Problems During High-Temperature Processing
Incomplete sealing occurs when part of the intended sealing area does not bond properly. This may result from insufficient heat, pressure, or dwell time, or from inconsistent contact between the sealing surfaces. The affected area may look closed but still contain a weak point.
Wrinkles across the seal can create channels through which liquid or air may pass. They often occur when the pouch opening is not positioned evenly, when the film is folded during sealing, or when the sealing area contains product residue.
Product contamination in the sealing zone is another common challenge. Sauces, oils, powders, and small food particles can interfere with direct contact between the sealant layers. Even a small amount of contamination may prevent a continuous bond.
Seal distortion or damage after retorting may indicate that the package experienced excessive stress, unsuitable processing conditions, or inadequate compatibility between the packaging structure and the process. However, a visual change alone does not prove that the seal has failed. Appropriate integrity testing is needed to establish the actual condition.
Recognizing these differences is more useful than treating every sealing issue as a general material defect.
How Filling Operations Affect Seal Quality
Many seal problems begin before a pouch enters the sealing machine. Filling operations determine how clean and consistent the sealing area remains.
When a pouch is filled too close to its opening, the product may spread onto the inner sealing surfaces. This is especially likely with viscous sauces, oily foods, and products containing small particles. If the residue is not removed, the sealing layers may not make uniform contact. The way a pouch is supported during filling also matters. An unstable pouch opening can fold, wrinkle, or shift, making it difficult to create a consistent seal. Operators should consider how the pouch is held, opened, filled, and transferred to the sealing station.
Fill quantity is another factor. Excessive filling can leave insufficient headspace and increase stress on the pouch during processing. It may also make it harder to keep the sealing zone clean. Consistent filling levels help reduce variation between packages.
For Retort Aluminum Foil Flat Pouches, a well-controlled filling process should therefore be treated as part of seal-quality management, rather than as a separate production step.
Controlling Heat, Pressure, and Sealing Time
Heat sealing depends on the interaction of temperature, pressure, and dwell time. These variables must work together to form a continuous bond between the compatible sealant layers.
If the temperature is too low, the sealant may not soften sufficiently to create a reliable bond. If it is too high, the material may become damaged, distorted, or weakened. Excessive pressure can also deform the sealing area, while insufficient pressure may leave gaps between the surfaces.
Dwell time affects how long heat and pressure are applied. A short sealing cycle may produce an incomplete bond, while an unnecessarily long cycle can damage the material. The appropriate settings depend on the pouch structure, sealing equipment, production speed, and actual operating conditions.
There is no universal temperature or pressure setting suitable for every retort pouch. Manufacturers should establish operating windows through equipment trials and packaging validation. Once suitable settings are confirmed, routine monitoring can help identify changes before they produce widespread defects.
Why Retort Compatibility Must Be Considered
A pouch that seals well before processing does not automatically maintain the same performance after retorting. High-temperature exposure can affect the sealant layer, adhesive system, and bonding between different laminate layers.
The packaging structure must be designed for the intended retort conditions. Materials that are suitable for ordinary flexible packaging may not be appropriate for high-temperature food processing. In addition, the structure must maintain its required mechanical strength and barrier performance after the complete thermal cycle.
The seal area deserves particular attention because it is formed by the inner sealant layers, while the rest of the pouch may contain several functional layers. A mismatch between the packaging structure and processing conditions can create weak points even when the overall pouch appears suitable.
When selecting Retort Aluminum Foil Flat Pouches, manufacturers should evaluate the complete package rather than focusing only on the aluminum foil layer. Sealant compatibility, laminate bonding, pouch construction, and the validated retort process all contribute to final performance.
Practical Checks for Reducing Seal Defects
- Before sealing: Confirm that the pouch opening is clean, flat, and correctly positioned. Check for product residue, wrinkles, and uneven folds in the sealing zone.
- During production: Monitor sealing temperature, pressure, dwell time, and equipment condition. Compare actual settings with the approved operating range and investigate unexplained changes.
- After retorting: Inspect representative pouches for leakage, seal distortion, punctures, and visible laminate damage. Use suitable integrity tests rather than relying on appearance alone.
- During storage and handling: Check whether stacking, compression, sharp edges, or rough transportation conditions place stress on the seal area.
Testing should reflect the intended application and relevant food-packaging requirements. Depending on the product and process, this may include seal-strength testing, leak detection, visual inspection, and other validated package-integrity methods. A passing visual inspection alone cannot establish that a pouch is safe or commercially sterile.
If a defect is found, affected products should be controlled according to the facility’s quality and food-safety procedures. Changes to the thermal process must be assessed by qualified personnel, since packaging adjustments cannot compensate for an inadequately validated food process.
Choosing Pouches for Reliable Sealing Performance
Reliable sealing begins with matching the pouch structure to the product and processing environment. Food type, filling temperature, viscosity, particle content, package dimensions, and retort conditions should all be considered before selecting a packaging format.
For product development, it is useful to evaluate the pouch as a complete system. The aluminum foil layer contributes barrier protection, while the inner sealant layer supports heat sealing and product contact. Other laminate layers contribute mechanical strength and help the package withstand handling and processing.
Packaging formats can also be tailored around filling equipment, required dimensions, printing, and storage needs. Working through these requirements with an experienced flexible packaging partner can help narrow down suitable structures and reduce avoidable compatibility problems. For Retort Aluminum Foil Flat Pouches, sample evaluation under representative filling, sealing, retort, and cooling conditions is an important step before large-scale production.
Conclusion
Seal problems in retort packaging can originate from filling contamination, uneven pouch positioning, unsuitable sealing conditions, or poor compatibility with high-temperature processing. Improving reliability requires attention to the entire production process, not simply increasing material thickness or changing one machine setting. By evaluating the laminate, sealing zone, equipment parameters, and finished-package integrity together, manufacturers can make more informed decisions and maintain consistent packaging performance.
FAQs
1. Can a retort pouch leak even if its seal looks normal?
Yes. Small channels or weak bonding areas may not be visible. Appropriate leak detection and seal-integrity testing are needed to assess the package.
2. What is the most common reason food contaminates the sealing area?
It often happens when filling levels are too high or when sauces, oils, and food particles reach the pouch opening during filling.
3. Does aluminum foil itself create a strong heat seal?
No. The inner sealant layer is responsible for forming the heat seal. Aluminum foil mainly provides barrier protection and must be combined with compatible packaging layers.
4. Should sealing settings be changed when a pouch fails after retorting?
Not automatically. First identify whether the issue comes from filling, sealing, material compatibility, retort conditions, or handling. Any process adjustment should be tested and validated before routine use.
Post time: Nov-03-2026